Carbon-Coated Aluminum Foil Production Process Flowchart
Sep 07, 2026
Carbon-Coated Aluminum Foil is the key material for the LIFP battery cathode collector; the production process mainly comprises two parts: manufacturing bare aluminum foil and manufacturing carbon-coated foil. Among them, carbon coating manufacturing is the core stage, covering slurry preparation, coating, drying, quality inspection, and post-treatment.
1.Bare aluminum manufacture(base material)
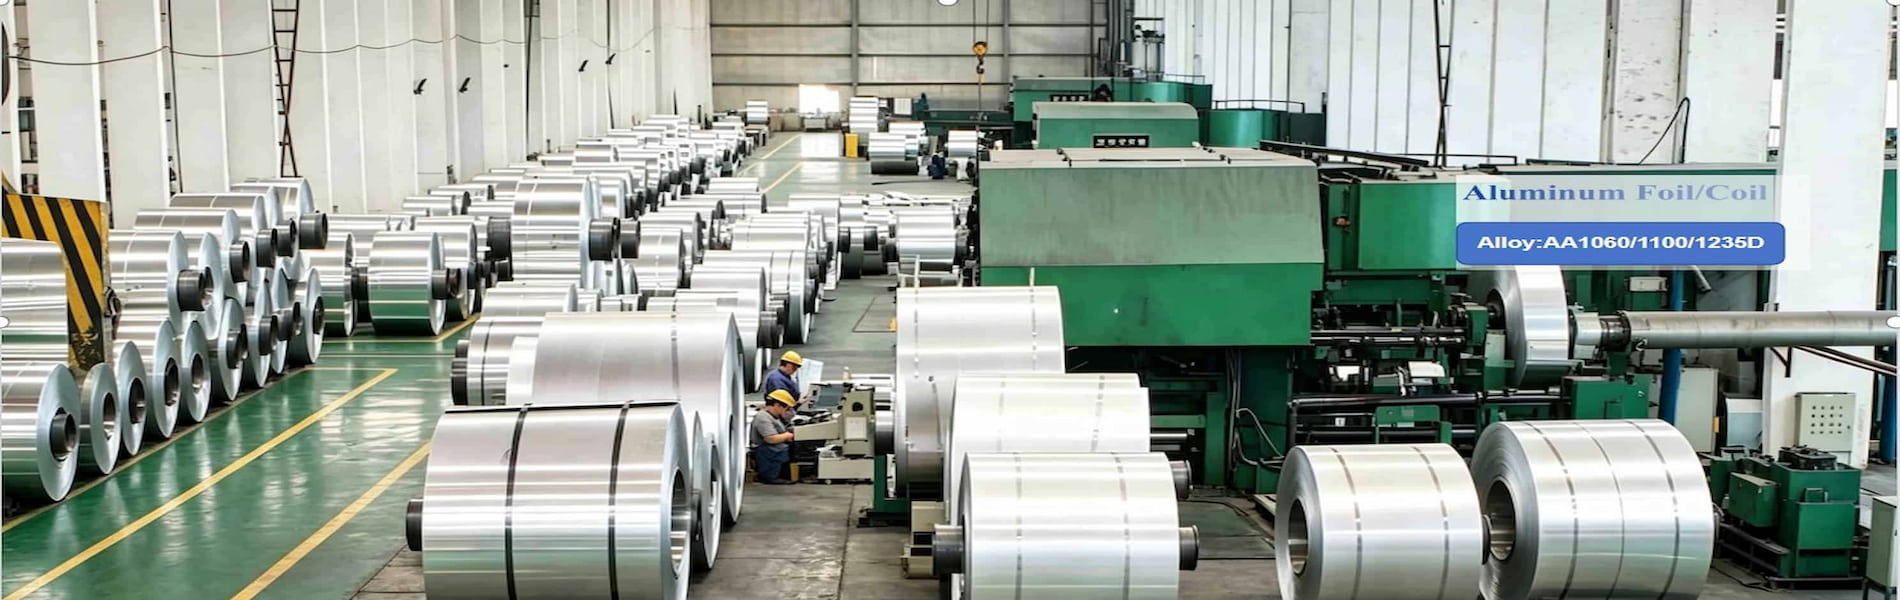
The basic material of carbon-coated aluminum foil is high-purity battery aluminum foil (purity over 99.9%, the ordinary thickness is 10-20um), primarily employing a cast-rolling–cold-rolling process.
Melting and homogenization: Aluminum ingots or billets are melted and cast into aluminum coils, followed by homogenization treatment to eliminate internal stresses and improve micro structural uniformity.
Hot rolling vs. cold rolling: Through multiple rolling processes—including hot rolling, cold rolling, intermediate annealing, and final rolling—the aluminum material is shaped to the specified dimensions, ensuring that the aluminum foil's thickness, surface roughness, and mechanical properties meet the required standards.
Surface treatment: The surface of bare aluminum foil usually has an oxide layer and oil, which need to be removed by alkaline cleaning, acid cleaning, ultrasonic cleaning, or corona treatment, among other methods, to achieve surface cleanliness and activation, improving the Subsequent carbon coating adhesion.
2. Carbon coating manufacture (core steps)
Carbon coating slurry preparation
Raw material ratio:
Mix conductive carbon materials (e.g., carbon black, graphite, carbon nanotubes, graphene, etc.) with a film-forming agent (e.g., PVDF, acrylate-based binders, etc.), a solvent (e.g., deionized water, isopropanol, etc.), and additives (e.g., dispersants, wetting agents, etc.) according to a specified proportion.
Dispersion and refining:
Mix and refine the material using a sand mill or high-speed disperser to control the slurry's viscosity, solid content, and particle size, ensuring the slurry is uniform, stable, and free from clumping.
Coating Process
Coating method:
The mainstream approach involves continuous roll-to-roll coating processes (such as gravure coating, blade coating, roller coating, or spray coating). Among these, gravure coating is the most widely used due to its ability to precisely control coating thickness (within ±0.5 μm) and its suitability for continuous manufacturing.
Parameter control:
The coating speed, the black between the aluminum foils, and the coating's tensile strength need to be controlled to ensure the slurry can be coated continuously and evenly on the aluminum foil.
Drying and solidification
Segmented drying and gradient curing:
After coating, the aluminum foil is placed into a multi-stage temperature-controlled oven (e.g., hot-air drying oven, infrared drying oven, or tunnel drying oven) for a gradient heating process that facilitates rapid solvent evaporation and preliminary curing of the carbon layer, thereby preventing coating cracking or blistering.
High-temperature curing:
In certain processes, the coated foil must undergo high-temperature curing in a curing oven; this high-temperature heating ensures complete curing of the carbon layer, thereby enhancing the adhesion strength between the coating and the aluminum foil as well as the stability of the conductive network.
Quality inspection
Before and after slitting, the finished product needs to be fully inspected, including Coating thickness measurement (thickness gauge), conductivity/rectangular resistance testing (resistance tester), adhesion testing (delamination test), and surface defect inspection (visual or optical inspection); reject any defects such as incomplete coating, scratches, or material detachment.
Post treatment
The aluminum foil, which has finished coating and solid process, goes through a cooling system and rectifies any deviation. Perform precise cutting using a cutting machine according to the battery manufacturer's specifications (e.g., narrow-width rolls). Finally, the product is wound onto a finished roll using a winding machine and then packaged with an anti-static/anti-moisture film.
Read More